Iron and steel industry decarbonization
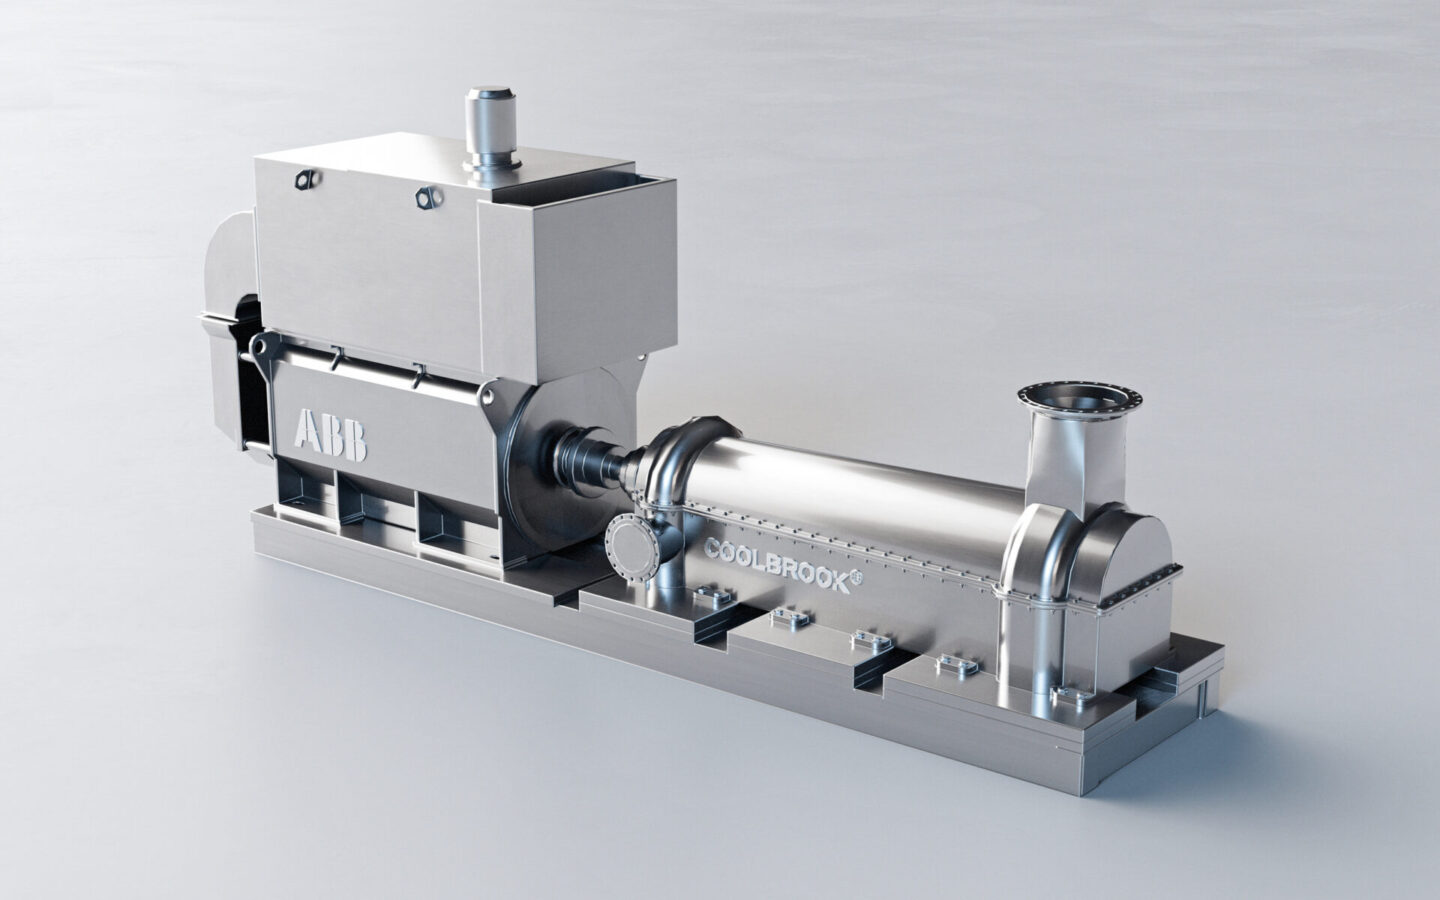
Coolbrook’s RotoDynamic Heater™ (RDH) replaces fossil-fuel heat in iron and steel production with clean electricity – from scrap and raw-material preheating to hot-stove air in the blast furnace, and later reduction gas for DRI and reheating furnaces.
Electrifying iron and steel production
The iron and steel industry produces around 7–9% of global CO₂ emissions. Much of it comes from coal and coke used to reduce iron ore, but a large share comes from burning fossil fuels for heat – in hot stoves, preheaters, reheating and heat-treatment furnaces. RDH heats air, nitrogen, CO₂, steam or process gases with electricity, and the hot gas replaces fuel firing in the process. In the blast furnace route it can also reduce coke consumption; in hydrogen-based DRI it raises energy efficiency by covering part of the heating duty. RotoDynamic Technology can cut up to 600 Mt of CO₂ a year in iron and steel at full deployment.
We develop steel applications with Tenova, a leading supplier of metals technology, and with steel producers including JSW and ArcelorMittal. In 2026 Business Finland granted funding for Coolbrook’s steel-industry development.
Key benefits
- No combustion emissions: no CO₂, NOx or SOx from fuel firing; zero CO₂ with renewable electricity
- Lower carbon and fuel costs: avoids fuel purchases and carbon-emission costs, and can use low-priced renewable power
- Efficient: 90–95% of the electricity becomes process heat; exhaust heat can often be recovered
- Available today in multi-megawatt scale with a path to scale to 50+ MW
- Compact: fits into new plants or retrofits into existing ones
The process
Where RDH fits in an iron and steel plant
Available now
Hot-stove air and fuel-gas preheating
(Blast Furnace)
RDH preheats combustion air or fuel gas (blast-furnace or coke-oven gas) for the hot stoves, so less gas is burned to heat the blast and temperature of gas entering hot stoves increases.
- Temperature: Ambient → up to 900 °C
- Benefits: Lower gas consumption in the hot stoves, lower coke use in the blast furnace and higher production capacity.
Scrap preheating
(EAF and BOF)
RDH supplies hot air to preheat scrap before it goes into the furnace.
- Temperature: Ambient → up to 800 °C
- Benefits: Shorter tap-to-tap time and higher throughput, with less electricity or fuel in the furnace.
Raw-material preheating
(Blast Furnace and DRI)
RDH preheats iron pellets and other raw materials before the ironmaking step.
- Temperature: Ambient → up to 900 °C
- Benefits: Lower coke use in the blast furnace and lower hydrogen use in hydrogen-based DRI.
Available later
Reduction gas heating
(DRI)
RDH heats hydrogen, natural gas or syngas for the direct-reduction shaft, directly or through a heat exchanger
- Temperature: 900 – 1,200 °C
- Benefits: Higher energy efficiency of hydrogen-based DRI.
Hot blast generation
(Blast Furnace)
RDH generates the hot blast directly, with the potential to replace the hot stoves.
- Temperature: Up to 1,400 °C
- Benefits: Significantly reduced coke consumption, higher production capacity, elimination of hot stoves altogether, significant avoidance of CO₂.
Reheating furnaces
(All routes)
RDH replaces burners in existing reheating furnaces, partly at first and fully later.
- Temperature: 1,200 – 1,500 °C
- Benefits: Electrifies one of the largest fuel users in the rolling mill.
Heat-treatment furnaces
(All routes)
RDH replaces burners in quenching, tempering, normalizing and annealing furnaces.
- Temperature: 500 – 1,400 °C
- Benefits: Fossil-free heat treatment with tighter temperature control.
Roadmap and process
Path to decarbonizing iron and steel processes
2026–27
First Applications
Blast Furnace:
- Preheating of hot stove air or fuel gas
- Preheating injection gas for tuyeres or shaft
- Preheating O2 and scrap for BOF
- Preheating raw materials
DRI:
- Preheating raw materials
- Indirect preheating of reduction gas (incl. hydrogen)
EAF (scrap route):
- Preheating scrap for EAF
All routes:
- Full or partial electrification of heat treatment furnaces
2030
Electrification of high temperature heat
Blast Furnace:
- Full replacement of hot stoves in BF
- Electrification of pellet induration & sintering
- Electrification of coking oven
DRI:
- Electrification of pellet induration
All routes:
- Electrification of reheating furnace
- Full electrification of heat treatment furnaces
2030+
Full decarbonization
Blast Furnace:
- CCS to capture process emissions from Blast Furnace and sintering processes to reach fully decarbonized operation
DRI:
- Direct preheating of reduction gas (incl. hydrogen)
Contact us
Hear from Coolbrook iron and steel customers and partners
JSW Group has set ambitious sustainability targets of reducing its specific CO2 emissions, aligning with the Sustainable Development Scenario of the International Energy Agency and India’s Nationally Determined Contributions. Deployment of RDH™ Technology is expected to have a sizeable impact on the decarbonization of the Group’s manufacturing process. We are happy to onboard Coolbrook as a partner on our journey to reduce CO2 emissions and achieve our climate targets.
PK Murugan, President
JSW Steel Vijayanagar & Salem Works